Minimal Space. Maximum Impact! Designed for when every millimeter matters> the new IRONLESS UNANO SERIES
Semiconductors
Increase throughput and precision of your system
Display
Enhance accuracy and precision with linear motors
Science and aerospace
Improve motion quality for a variety of applications
Machine tooling
Robust solutions for increased speed and precision
Digital cutting
Create modular and high throughput applications
Printing
Increase printing speed and quality using linear motors
Robotics
Integrate compact solutions for guaranteed uptime and high dynamics
Life science
Establish precise and clean integrated solutions
Woodworking
Maximize performance and accuracy for high throughput
Stages and system solutions
Compact integration and high performance for your axis
Vacuum applications
Best performance for clean and vacuum applications
Characteristics
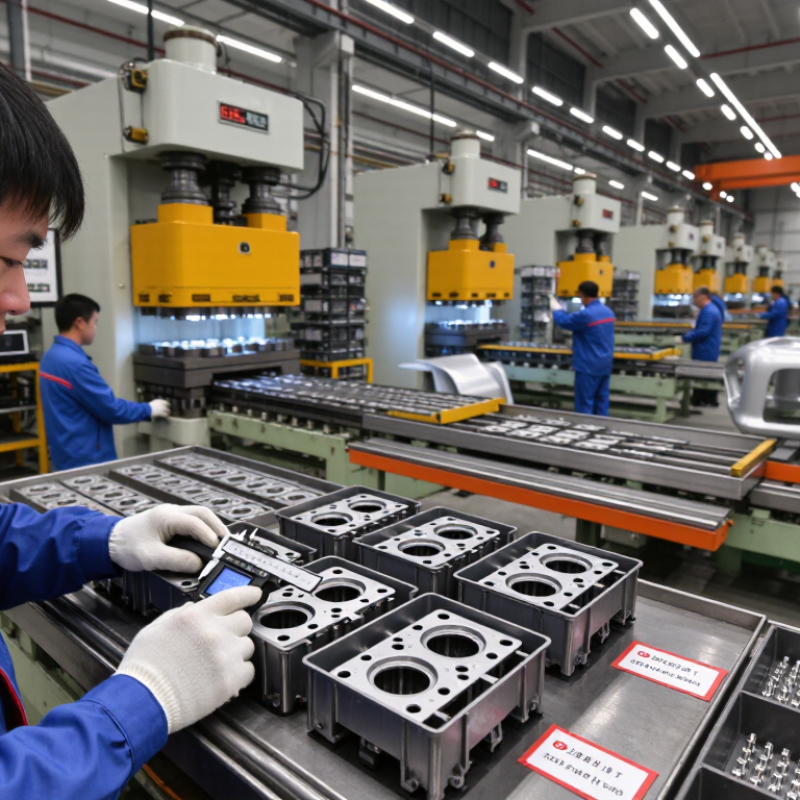
China’s metal stamping sector serves automotive, appliance, electronics, and industrial buyers with parts ranging from tiny contact terminals to deep-drawn housings. Scale matters, but it is not proof of fit. A buyer still needs evidence of tooling capability, material control, dimensional inspection, and stable production across repeat orders. The details show quickly: a burr on a stamped edge, a misaligned hole, or a springback issue can disrupt assembly.
Grand View Research estimated the global metal stamping market at USD 218.3 billion in 2023 and forecast a 4.3% compound annual growth rate from 2024 to 2030. This is a useful market signal, not a supplier scorecard. Metal-forming researcher Taylan Altan’s published work emphasizes that successful forming depends on understanding material behavior alongside tooling and process design. That principle matters when evaluating manufacturers in China: ask how they validate dies, inspect first articles, and respond when a drawing changes. A polished catalog cannot answer those questions. Request sample parts and review the inspection records. There is no perfect supplier. Even a capable factory may need time to stabilize a new tool, and buyers should leave room for that reality. This guide compares manufacturers through practical criteria, helping global buyers narrow the field without treating price or production capacity as the whole story.
China’s metal stamping sector serves buyers who need repeatable parts, from small brackets to formed electrical contacts. Common processes include blanking, piercing, bending, and progressive-die stamping. Each suits different geometries and production volumes. A sharp edge on a pierced hole may affect assembly, while springback can shift a bend angle. These details deserve attention before tooling begins.
Material choice changes both performance and cost. Carbon steel offers strength; stainless steel resists corrosion; aluminum reduces weight; copper supports electrical conductivity. Thickness, temper, grain direction, and surface coating also influence forming behavior. Buyers should compare sample parts against drawings and review inspection records, not just quoted prices. Ask how the supplier controls burrs, dimensions, and tool wear across production runs. A polished sample is useful, but it cannot prove long-term consistency. In practice, no checklist catches everything; unclear drawing notes can still create delays.
Tips: Send complete drawings and expected volumes. Confirm tolerances, finish, packaging, and sampling plans in writing. Request a production sample before approving a full run. Small checks help. Also discuss how design changes will be documented, since even a minor revision can affect tooling and fit.
Reliable stamped parts begin with controlled operations. Blanking cuts a flat outline from sheet metal; piercing creates holes for fasteners, vents, or alignment pins. Tool clearance affects edge quality, while burr direction matters during assembly. A useful inspection checks hole position, burrs, and the part’s outline. Small errors travel.
Bending forms flanges and channels, but springback can shift an angle after the press opens. Deep drawing pulls a flat blank into a cup or enclosure. Die radius, lubrication, and blank-holder force help control wrinkles and thinning. The awkward part? Material lots can behave differently. Even a sound setup may need adjustment.
The International Energy Agency’s Global EV Outlook 2024 reports nearly 14 million electric-car sales in 2023, about 18% of global car sales. That growth supports demand for stamped body and battery-enclosure parts, though the report does not measure stamping volumes. The World Steel Association reported 1,888.2 million tonnes of crude-steel production in 2023; not all of it becomes stamping-grade sheet. Buyers should therefore assess material traceability alongside process capability, sample dimensions, and production consistency. No single inspection tells the whole story.
For global buyers, a metal stamping supplier’s quality claims should be checked against working records. ISO 9001:2015 indicates a documented quality management system, while IATF 16949:2016 adds requirements for automotive production and related supply chains. Neither certificate proves that every stamped part will meet your drawing. Ask to see how the supplier controls material certificates, die changes, inspection results, and nonconforming parts. A sample audit can reveal gaps that a certificate alone may not show.
PPAP helps verify that a production process can repeatedly make parts to specification. Its 18 elements may include design records, process flow, PFMEA, control plans, measurement studies, dimensional results, and the Part Submission Warrant. Not every program requires every element; confirm the required submission level and customer-specific requirements before approving tools. Look closely at trial-run data, not just the completed forms. A neat binder can still hide unstable dimensions.
Tips: Request a traceable sample lot and compare its inspection report with your drawing. Check that gauge calibration is current and that corrective actions include evidence of effectiveness. Ask who approves process changes. Small details matter. If a supplier cannot explain a control plan in plain language, pause and investigate.
| Assessment Area | Requirement or Evidence | What Buyers Should Verify |
|---|---|---|
| Quality Management Systems | ISO 9001:2015 certification | Check the certificate’s validity, certified legal entity, manufacturing-site address, scope, and certification body. Certification indicates an audited quality management system; it does not guarantee that every part or shipment will be defect-free. |
| Quality management system scope | Confirm that the scope covers the relevant activities, such as metal stamping, tooling, inspection, and any associated manufacturing processes performed at the proposed site. | |
| Risk-based planning and operational controls | Review how the supplier identifies process risks, controls production changes, manages nonconforming outputs, and evaluates corrective-action effectiveness. | |
| IATF 16949:2016 certification, when applicable | For automotive supply, verify the certificate and site against the applicable IATF database or certification-body records. Confirm that the product and manufacturing scope are relevant to the program. | |
| Customer-specific requirements | Confirm that the supplier has identified and applies the buyer’s applicable requirements, including submission, traceability, change-notification, and approval rules. | |
| Metal Stamping Process Capability | Press and process suitability | Compare press tonnage, stroke, bed dimensions, shut height, feed capability, and process type with the part, die, material, and production-volume requirements. |
| Tooling and die management | Review die design and maintenance records, preventive-maintenance plans, repair history, spare-part controls, and ownership or transfer arrangements. | |
| Material control and traceability | Check material specifications, supplier certificates or test reports where required, incoming inspection, lot identification, and traceability through production and shipment. | |
| Process monitoring and inspection | Review control plans, inspection methods, sampling frequency, reaction plans, and records for critical dimensions and characteristics identified by the customer. | |
| Measurement system and laboratory controls | Verify that measuring equipment is calibrated and suitable for its intended use. Review measurement-system studies and laboratory qualifications where required by the customer or submission level. | |
| PPAP: 18 Elements | 1. Design Records | Current drawings, specifications, and other applicable design records for the part; confirm revision alignment with the customer-approved definition. |
| 2. Authorized Engineering Change Documents | Approved engineering changes not yet incorporated into the design record, if any; verify authorization and effectivity. | |
| 3. Customer Engineering Approval | Customer engineering approval, if required for the part, process, or design change. | |
| 4. Design Failure Mode and Effects Analysis (DFMEA) | Applicable where the supplier is responsible for design; review design-related risks and actions. If design responsibility rests with the customer, follow the customer’s applicable requirements. | |
| 5. Process Flow Diagram | Document the production process sequence, including relevant incoming, manufacturing, inspection, and shipping steps. | |
| 6. Process Failure Mode and Effects Analysis (PFMEA) | Review process failure modes, effects, causes, controls, and actions for the production process. | |
| 7. Control Plan | Confirm that controls, measurement methods, sample sizes or frequencies, and reaction plans address the applicable process and product characteristics. | |
| 8. Measurement System Analysis (MSA) Studies | Review applicable measurement-system studies, such as gauge repeatability and reproducibility, in accordance with customer requirements. | |
| 9. Dimensional Results | Check dimensional inspection results for the required samples and characteristics against the current drawing and specifications. | |
| 10. Material, Performance Test Results | Review required material and performance test results, including applicable test methods, specifications, and laboratory records. | |
| 11. Initial Process Studies | Review initial process capability or performance studies for designated characteristics when required by the customer. | |
| 12. Qualified Laboratory Documentation | Provide evidence of laboratory qualification or accreditation when required for the laboratory performing specified tests. | |
| 13. Appearance Approval Report (AAR) | Submit an AAR when the part has applicable appearance requirements and the customer requires approval. | |
| 14. Sample Production Parts | Provide production-representative samples made using the intended production process, tooling, materials, and conditions as required. | |
| 15. Master Sample | Identify and retain an approved master sample when required; confirm its identification and retention controls. | |
| 16. Checking Aids | Document applicable fixtures, templates, models, or other checking aids, including their calibration or verification controls. | |
| 17. Records of Compliance with Customer-Specific Requirements | Provide the records needed to demonstrate compliance with the customer’s applicable PPAP and program-specific requirements. | |
| 18. Part Submission Warrant (PSW) | Review the completed warrant for correct part and revision identification, submission reason, results, and authorized approval. | |
| Submission and Approval | PPAP submission level and applicability | The customer determines the required submission level and applicable evidence. Confirm the submission scope, timing, approval status, and any required re-submission triggers with the customer before production release. |
When comparing metal stamping manufacturers, start with the part, not the largest press number. Press capacity must suit the material, thickness, forming depth, and die size. A 300-ton press can be a poor fit if its bed or stroke cannot handle your tool. Ask for the machine range and examples of comparable parts. Numbers need context.
Tooling capability affects both quality and launch timing. Check whether the manufacturer designs, builds, maintains, and modifies dies in-house or through qualified partners. Request a tooling plan, trial schedule, and clear ownership terms. Then review tolerance control: stamped dimensions can shift with material variation, tool wear, and springback. A tolerance is only useful when the measurement method and inspection frequency are defined. Check the evidence.
Production volume changes the right choice. A shop suited to short runs may offer flexibility, while high-volume work demands stable cycle times, planned maintenance, and enough capacity for repeat orders. Ask for production records or trial-run data, not just a quoted monthly output. I would not treat one approved sample as proof of long-term consistency; that assumption is easy to make. Compare scrap tracking, inspection reports, and how issues are corrected. A thoughtful supplier should explain trade-offs plainly, including where a tighter tolerance raises tooling or inspection demands.
Indicative press-capacity bands for common press classes—not specifications or verified claims for individual manufacturers.
How to compare suppliers: Press capacity is only one factor. Confirm tooling type and ownership, achievable tolerances for your material and part geometry, and expected annual production volume against your drawings and order forecast. Tolerances should be agreed in the part specification and verified using an appropriate inspection and capability plan.
Capacity bands are broad industry reference ranges; equipment classifications and actual capabilities vary by supplier and application.
For global buyers, a metal stamping quote is only the starting point. A capable manufacturer should explain how it verifies material and process requirements. Ask for current RoHS test reports and material declarations, then check that product descriptions and revision dates match your parts. REACH information needs similar care: confirm which substances and product categories the documentation covers. A certificate alone may not answer every question. Details matter.
Traceability should connect each shipment to a production lot, material batch, and inspection record. Request a sample record before placing a large order. Can the supplier identify the steel grade, stamping date, and inspection results from one carton label? During a factory review, compare those records with actual labels and packing documents. Gaps happen. The useful question is whether the supplier finds and corrects them openly.
Export logistics affect quality, too. Ask how parts are protected from moisture, scratches, and shifting during transit. Clarify carton dimensions, pallet standards, shipping terms, and who prepares export documents. A small stamped bracket can still arrive bent if cartons are stacked poorly. Request a trial shipment when order volumes justify it, and review delivery timing against real transit records. Some processes may look tidy on paper but remain inconsistent on the shop floor. Verify both.